

The Application Value of Ball Mills
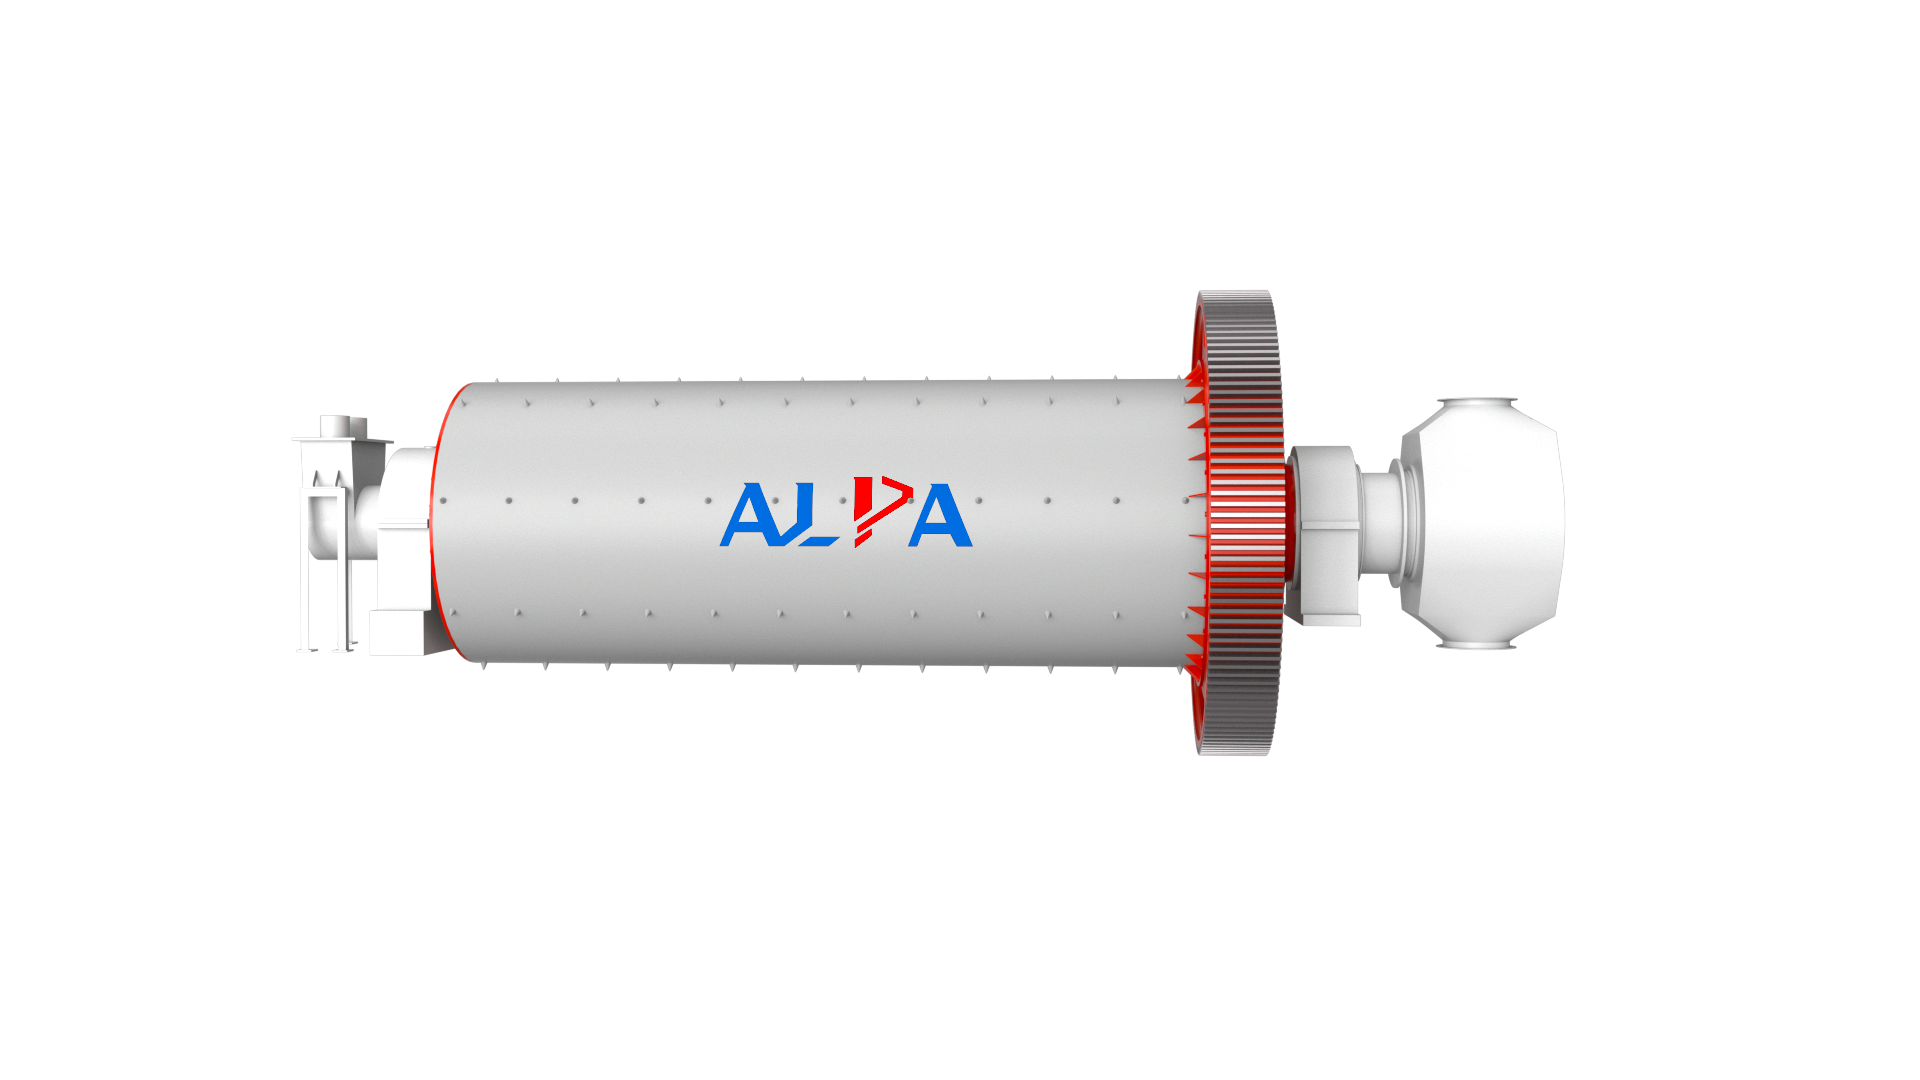
With the rapidly growing demand for fine particles in sectors such as the food and fine chemical industries, ultrafine grinding technology has garnered significant attention. Common ultrafine grinding techniques include jet milling, colloid milling, and ball milling. Among these, ball milling—a process that utilizes mechanical energy and thermal effects—alters the structure and properties of materials through friction, collision, and shear. It offers several advantages, including high product stability, superior processing quality, low costs, and an environmentally friendly, pollution-free operation; consequently, it is widely employed for the pulverization of a diverse range of materials, including minerals, food products, pharmaceuticals, and chemicals.
The operating principle of a ball mill primarily involves the rotation of material around the mill's central axis, while the supporting plate rotates in the opposite direction. The combination of these two rotational speeds generates a centrifugal force that subjects the sample to intense friction and shear, resulting in ultra-fine particle size.
Based on their specific operating principles and characteristics, ball mills are generally categorized into three types: stirred (agitated) ball mills, vibratory ball mills, and planetary ball mills.
A vibratory ball mill utilizes high-frequency, simple harmonic vibration of the grinding chamber to induce vigorous impact, compression, and shear stress between the grinding media and the material, thereby enabling rapid size reduction and uniform mixing. Typically, such mills can reduce material to the micrometer (micron) scale.
Ball milling processes are categorized into dry and wet methods, depending on whether a liquid dispersion medium is added during the grinding process. In dry ball milling, dry materials are loaded directly into the mill; this approach offers advantages such as a streamlined process, ease of operation, and lower energy consumption, making it widely used in traditional sectors like food processing. Wet ball milling, by contrast, requires the addition of a dispersion medium to the material, with size reduction achieved through the friction, collision, and impact forces generated between the grinding media and the material. Although wet ball milling involves more complex process parameter control and operating conditions—often necessitating the use of grinding aids—the equipment itself is relatively simple in design, and it yields a highly uniform product. Whether dry or wet, the ultrafine grinding process utilizes powerful shear, impact, and collision forces to transform food raw materials into powders of varying particle sizes, thereby meeting a diverse range of application requirements.
There is a wide variety of ball mill types, and the milling outcome is influenced by numerous factors, such as the density of the grinding media, the number and size of the grinding balls, milling speed, milling duration, temperature, the ball-to-powder ratio, and the filling ratio. Due to the interplay of these variables, the energy delivered by a ball mill can vary significantly. Low milling energy results only in particle size reduction and an increase in specific surface area; however, high energy (high-energy ball milling) can lead to the breaking of chemical bonds and the initiation of chemical reactions. Therefore, the optimal milling conditions must be determined based on the desired outcome.
As a core method for ultrafine grinding, ball milling—leveraging the synergistic effects of intense mechanical force and thermal energy—has become an increasingly significant focus in the advanced processing of food. Its applications have expanded well beyond conventional size reduction to encompass the release of functional components, the modification of dietary fibers, and the enhancement of bioactive substances. Extensive research indicates that ball milling can significantly alter the physicochemical and functional properties of the processed materials. With the ongoing integration of intelligent equipment and a deeper understanding of the underlying process mechanisms, ball milling holds vast potential for applications such as the precise release of functional food components, the development of novel raw materials, and the comprehensive utilization of by-products.
Anhydrous Dicalcium Phosphate: Its Importance in These Three High-Value Sectors
Anhydrous dicalcium phosphate (DCPA) is an important inorganic functional material widely used in fields such as pharmaceuticals, bone repair, and food additives. In the pharmaceutical industry, DCPA primarily serves as a filler, diluent, and auxiliary disintegrant for tablets and capsules. In the field of bone repair, it can exist either as a single phase or in combination with other calcium phosphate phases; as a novel material for repairing bone defects, it shows great promise for biomedical applications. In the animal feed sector, DCPA acts as a highly efficient dual-source calcium and phosphorus supplement, promoting skeletal development and enhancing the production performance of livestock and poultry. In the food industry, it is commonly used as a nutritional fortifier and anti-caking agent. Given this diverse range of applications, DCPA is attracting increasing attention from researchers.
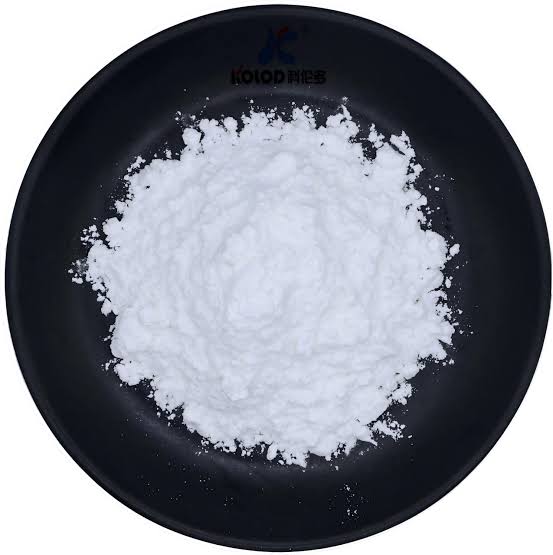
Anhydrous dicalcium phosphate (DCPA) appears as an odorless, tasteless white powder and exists in a triclinic crystalline form (also known as monetite). Its unit cell is held together by a combination of three types of hydrogen bonds and Ca-O bonds. It is virtually insoluble in water or ethanol but readily soluble in dilute hydrochloric or nitric acid. Stable at room temperature, it is non-hygroscopic and does not undergo phase transitions or hydration to form the dihydrate; however, it converts to calcium pyrophosphate at high temperatures. The primary deformation mechanism of DCPA is brittle fracture, which reduces strain sensitivity and facilitates the transition from laboratory-scale trial production to industrial-scale application.
The global market for anhydrous dicalcium phosphate continues to expand steadily, with a projected compound annual growth rate of 5.5% over the next five years. Growth is driven primarily by three key downstream sectors: animal feed, pharmaceuticals, and food.
The animal feed sector accounts for the largest share; as a highly efficient calcium and phosphorus supplement, the product's core function of promoting skeletal development and enhancing the productivity of livestock and poultry drives sustained demand alongside the global rise in meat consumption, while the trend toward quality upgrading further boosts usage volumes.
Although the pharmaceutical sector represents a relatively smaller market share, it offers high product value-added and significant growth potential. High-purity, pharmaceutical-grade anhydrous dicalcium phosphate is widely used in oral solid dosage forms as a filler, disintegrant, and dissolution enhancer, playing a particularly crucial role in improving the bioavailability of poorly soluble drugs. Driven by the expansion of the global generic drug market, advancements in novel formulation technologies, and increasing demands for patient medication adherence, the demand for pharmaceutical-grade products continues to rise, creating structural opportunities within the market.
From a regional perspective, the Asia-Pacific region—led by China—is emerging as the fastest-growing market for anhydrous dicalcium phosphate globally, benefiting from a massive livestock industry, a rapidly developing pharmaceutical sector, and a continuously upgrading consumer market.
Thanks to its high purity, excellent biocompatibility, and stable physicochemical properties, anhydrous dicalcium phosphate demonstrates irreplaceable value in applications such as pharmaceutical excipients, bone repair materials, and feed additives. Looking ahead, the market potential for anhydrous dicalcium phosphate is poised for further expansion, driven by the convergence of several factors: rising demand for bone health solutions amidst an aging population, the booming development of generics and biologics, and the large-scale expansion of global livestock and poultry farming.
What are the medicinal uses of talcum powder?
Talc powder is a common white, powdery silicate substance; when finely purified, it is colorless, odorless, and exceptionally safe. Highly versatile and adaptable, it serves not only as a direct medicinal ingredient but also as a key raw material in traditional Chinese medicine processing and cosmetics manufacturing, playing an integral role in daily life as well as in the pharmaceutical and beauty industries. Below, we provide a detailed breakdown of the core properties and medicinal value of talc powder for those interested in learning more.
Benefits and Functions of Talc Powder
1. Clearing Heat and Relieving Summer-Heat
Talc powder possesses properties that help clear internal heat-toxins. It is particularly suitable for use during the summer and is effective in treating heatstroke caused by hot weather; it can be used in combination with herbs such as raw licorice and *Eupatorium* (Peilan). Additionally, when prickly heat causes pain and itching in the summer, talc powder can be applied directly to the affected area, providing noticeable relief from pain and itching.
2. Relieving Diarrhea
Talc powder has significant astringent properties; it clears internal damp-heat and eliminates intestinal inflammation. It is effective in treating diarrhea caused by the invasion of heat-toxins and can be taken in combination with medicinal herbs such as plantain seeds (*Cheqianzi*) and *Poria* (*Fuling*). It can also be taken with plantain seeds and *Akebia* stem (*Mutong*) to promote diuresis and alleviate symptoms such as difficult urination or bodily edema.
3. Protecting Gastrointestinal Mucosa
When used medicinally, talc powder benefits the gastrointestinal mucosa. Beyond clearing heat, detoxifying, and reducing inflammation, it helps stop vomiting and diarrhea while protecting the mucosa from bacterial and viral damage. It also aids in repairing damaged gastrointestinal lining, offering relief for conditions such as acute or chronic gastritis and gastric ulcers.
Medicinal Value of Talc Powder
Talc powder is highly valued in Traditional Chinese Medicine, particularly for treating eczema. It is often formulated into a medicinal solution—sometimes combined with calamine—and applied directly to the affected areas. Frequent application can help resolve eczema and rapidly alleviate the associated pain and itching.
Functional Characteristics of Seven Common Categories of Dispersants
A dispersant is an amphiphilic polymer containing both hydrophilic and hydrophobic structures; it stabilizes the dispersion of solids or liquids within incompatible media through mechanisms such as electrostatic repulsion or polymer steric hindrance, ensuring that the hydrophilic and hydrophobic groups within the molecule function effectively.
Dispersants have a wide range of applications and come in many varieties; they are primarily categorized into seven major types: anionic, cationic, non-ionic, amphoteric, electrically neutral, polymeric, and hyper-dispersants.
Anionic Dispersants
Based on cost-effectiveness and dispersion performance, anionic dispersants are considered promising additives widely used in industry.
Anionic dispersants consist of two structural components: a negatively charged hydrophilic group and a lipophilic hydrocarbon chain.
Cationic Dispersants
The molecular structure of cationic dispersants typically comprises two parts: a positively charged hydrophilic group and a lipophilic hydrocarbon chain; compounds formed from these two parts constitute cationic surfactants.
Cationic dispersants exhibit exceptionally strong adsorption on material surfaces and are widely used with pigments such as carbon black and organic pigments.
Non-ionic Dispersants
Non-ionic dispersants are composed of compounds that neither ionize nor carry an electric charge. While they can reduce surface tension and improve wettability—and their dispersing power is generally weaker than that of ionic (anionic/cationic) dispersants—they still deliver excellent dispersion results in specific systems or materials, such as pH-sensitive dispersion media, multi-charged systems, and organic solvents.
Currently, the most common non-ionic dispersants on the market—which see widespread application—include fatty acid ethylene oxide adducts (R-COO(CH2CH2O)nH), polyethyleneimine derivatives ((NHCH2CH2)nNH2), and polyethylene glycol polyols (HO(CH2CH2O)nH).
Amphoteric Dispersants
Amphoteric polymers, also known as polyampholytes, contain repeating units of both cationic and anionic monomers.
Common amphoteric dispersants include carboxylates and sulfonates; among carboxylate-type dispersants, the amino acid type and the betaine type are the most prevalent.
Electroneutral Dispersants
The fundamental characteristic of electroneutral dispersants is that the sizes of the anionic and cationic organic functional groups are roughly equal; the molecule as a whole is electrically neutral yet possesses polarity.
Oleylamino oleate is a common electroneutral dispersant on the market and enjoys a strong application profile. Polymeric DispersantsAs a specific class of polymers, polymeric dispersants are characterized by high molecular weights and excellent dispersing capabilities. These properties stem primarily from the presence of both hydrophilic and hydrophobic groups within their molecular structures.Common types of polymeric dispersants include (meth)acrylic acid and (meth)acrylate copolymers, as well as low-molecular-weight polyethers derived from polyhydroxystearic acid. Their molecular structures can be constructed in three ways: grafting hydrophobic chains onto a hydrophilic backbone, grafting hydrophilic chains onto a hydrophobic backbone, or arranging hydrophilic and hydrophobic segments in an alternating pattern.
Hyperdispersants
Hyperdispersants are block copolymers featuring multiple anchoring groups within their molecular structure. They provide excellent wetting and dispersion on pigment surfaces—proving particularly effective for hard-to-disperse pigments such as titanium dioxide and phthalocyanine blue—and significantly enhance properties like coating fluidity, gloss, and adhesion, largely due to the strong affinity they establish with the pigment surface.
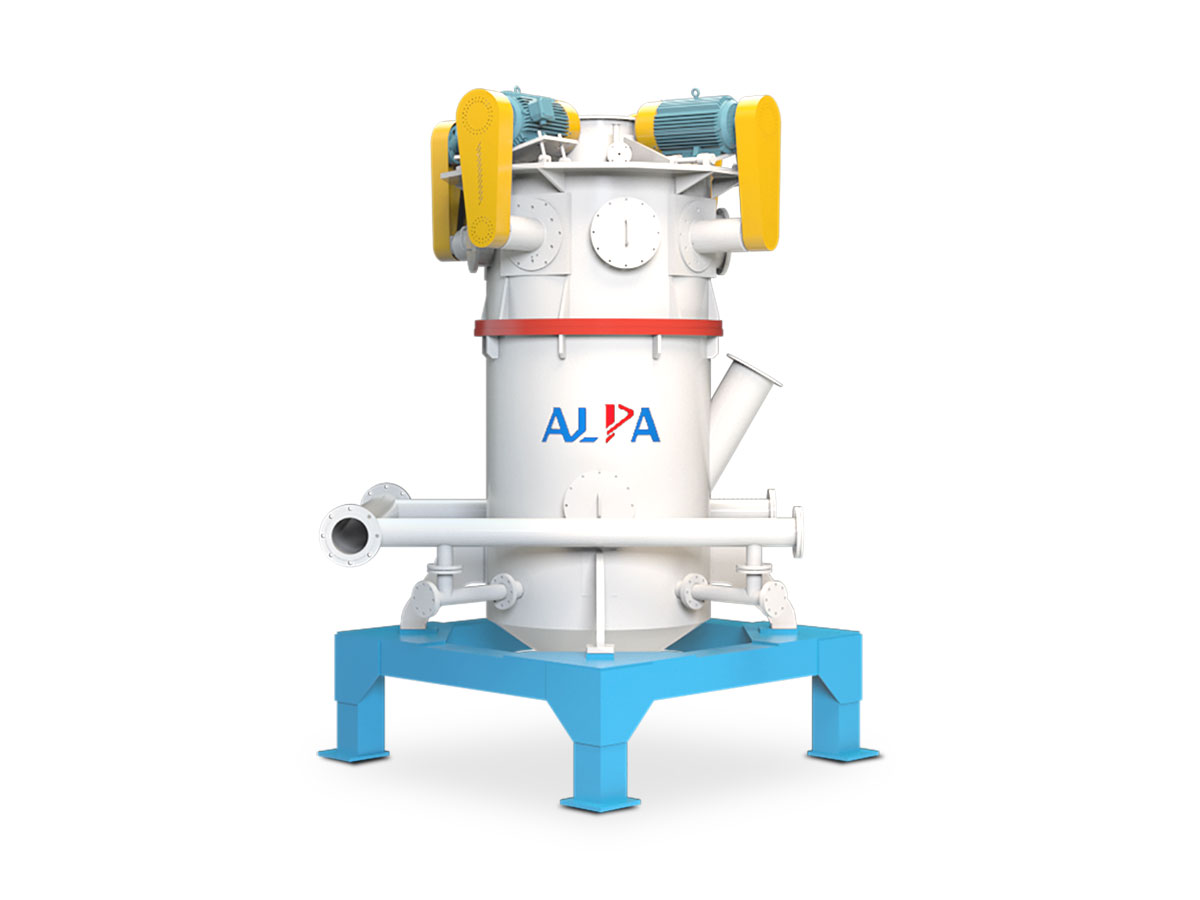
How do you choose a jet mill for pulverizing lithium salts?
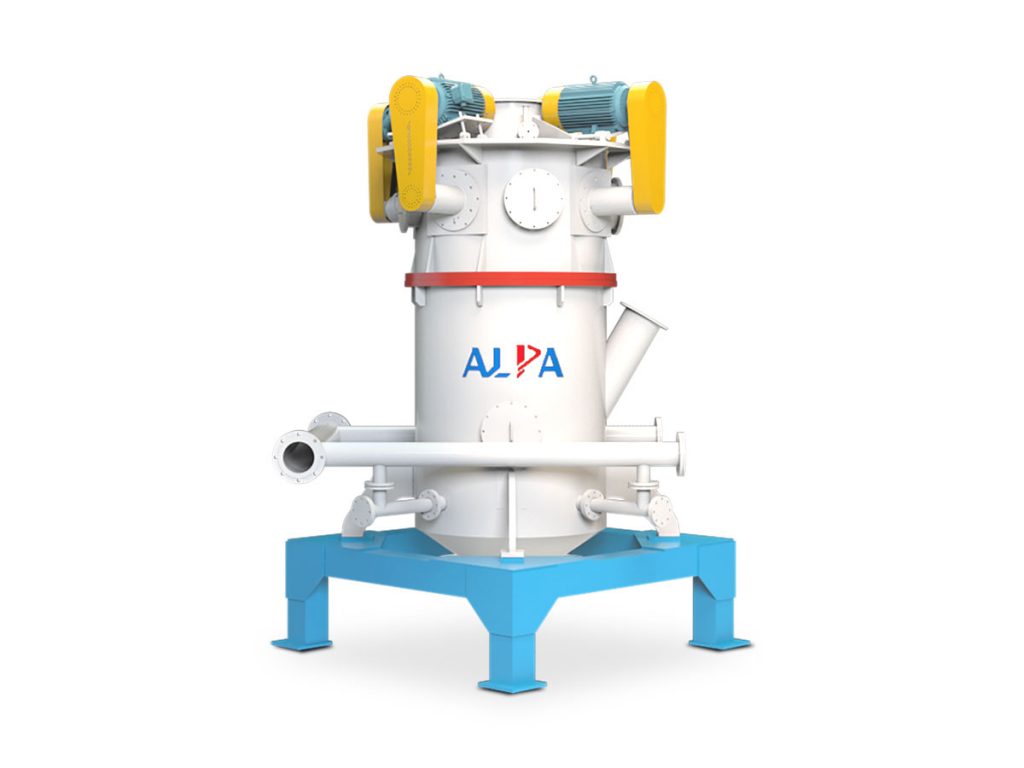
The jet mill is a critical piece of equipment for ultrafine pulverization, capable of reducing materials to powders with particle sizes in the micrometer range. Also known as an air jet mill or fluid energy mill, it utilizes high-speed gas streams or superheated steam to pulverize materials through inter-particle collisions, friction, and shearing. In the new energy battery materials sector, manufacturers of battery-grade lithium salts must further pulverize crystallized and dried lithium carbonate or lithium hydroxide products to meet the processing requirements of downstream lithium battery manufacturers. Currently, the industry primarily employs jet mills to pulverize dried battery-grade lithium salt particles to achieve the required product particle size specifications.
Given the production characteristics of battery-grade lithium salts, the prevailing equipment design is the fluidized-bed type. By installing a classifier at the outlet of the fluidized-bed jet mill, the synergistic action of the fluidized bed and the classifier ensures that the lithium salt product meets user specifications regarding particle size and particle size distribution.
The working principle of the fluidized-bed (opposed-jet) jet mill involves directing gas through a set of nozzles (more than two) to create an opposed-jet flow field within the grinding chamber, thereby fluidizing the material. At the intersection point of the nozzle jets, particles undergo intense collisions, friction, and impact, resulting in pulverization. Under negative pressure, the pulverized powder passes through the classifier; product meeting specifications is collected by a cyclone separator and dust collector, while coarser particles that do not meet requirements fall back into the grinding zone under gravity for further processing.
Compared to other pulverizers, fluidized-bed jet mills offer advantages such as a narrow particle size distribution, high grinding efficiency, low energy consumption, minimal product contamination, and low wear on components; however, the initial equipment cost is relatively high. Since the material must be fluidized to be pulverized by the colliding gas jets, these mills typically require the feed material to possess a certain degree of fineness—a requirement that is particularly critical for high-density materials.
As an effective ultra-fine grinding technology, jet milling has become a crucial stage in the production of battery-grade lithium salts. The commissioning of jet milling equipment demands a high level of technical expertise and professionalism; during operation, users should ensure sufficient material residence time, maintain stable air supply pressure, and strictly adhere to operating procedures to achieve optimal grinding performance, thereby reducing energy consumption and ensuring consistent product quality.
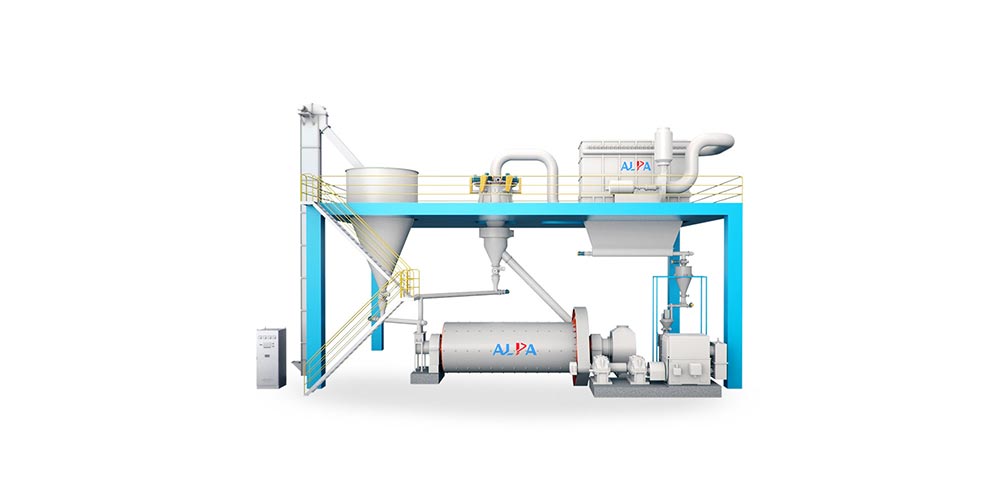
Grinding particles enhance value
With the rapidly increasing demand for fine particles in industries such as food and fine chemicals, ultrafine grinding technology has attracted widespread attention. Common ultrafine grinding technologies include air jet milling, colloid milling, and ball milling. Among them, ball milling is a method that utilizes mechanical energy and thermal effects to change the structure and properties of materials through friction, collision, and shearing. It has the advantages of stabilizing samples, producing high-quality products, low cost, and being environmentally friendly and pollution-free, and is widely used in crushing various minerals, food, pharmaceuticals, and chemical materials.
The working principle of a ball mill is mainly that the material rotates around the rotating shaft of the ball mill, while the support plate rotates in the opposite direction. The combination of these two speeds generates a certain centrifugal force, which makes the sample undergo sufficient friction and shearing, thereby achieving an ultrafine state.
Ball milling processes can be divided into dry and wet methods, depending on whether a liquid dispersion medium is added during the grinding process. Dry ball milling directly feeds dry materials into the mill for grinding, offering advantages such as a short process, simple operation, and low energy consumption, making it widely used in traditional fields such as grain processing. Wet ball milling, on the other hand, requires the addition of a dispersion medium to the material, utilizing the friction, collision, and impact between the grinding medium and the material to achieve pulverization. Although the process parameters and operating conditions of wet ball milling are more complex, often requiring the addition of grinding aids, its equipment structure is relatively simple, and the product exhibits good grinding uniformity. Regardless of whether it is a dry or wet method, the ultrafine grinding process can process food raw materials into powders of different particle sizes through powerful shearing, impact, and collision forces, thereby meeting diverse application needs.
There are many types of ball mills, and the ball milling effect is affected by multiple factors, such as the density of the grinding material, the number and size of the grinding balls, grinding speed, grinding time, grinding temperature, ball-to-material ratio, filler ratio, etc. Due to the combination of these variables, the energy delivered by a ball mill varies greatly. If the grinding energy provided is low, only changes in particle reduction and specific surface area increase will occur; but if the energy is high (high-energy ball milling), the decomposition of chemical bonds and the occurrence of chemical reactions can be achieved. Therefore, depending on the desired effect, the optimal grinding conditions must be determined.
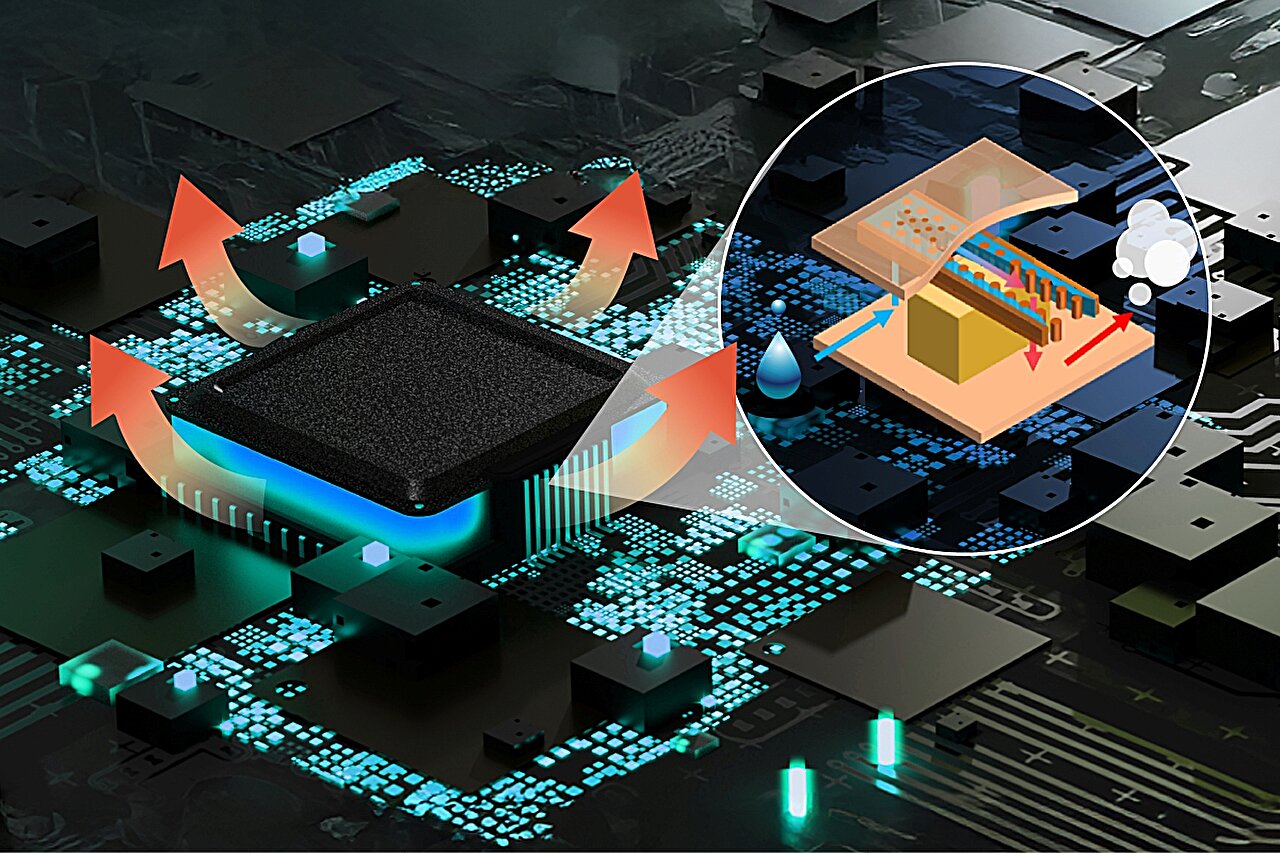
Application of Diamond Powder in Heat Dissipation for High-End Chips
With the rapid evolution of AI computing power and the mounting thermal management challenges facing high-end chips, diamond—a material with exceptional thermal conductivity—is emerging as a promising new semiconductor material.
Diamond’s superior thermal conductivity stems from its unique microstructure, where heat transfer relies primarily on lattice vibrations. The extremely high bond energy of the C-C bonds and the low mass of the carbon atoms restrict atomic vibration to the vicinity of the potential energy minimum; this characteristic imparts an exceptionally high thermal conductivity to the material. Simultaneously, because all valence electrons in diamond are involved in bonding and cannot move freely, the material acts as an excellent electrical insulator. This combination of high thermal conductivity and electrical insulation significantly broadens its potential applications.
Micron- or nano-scale diamond powders—characterized by a narrow particle size distribution, favorable morphology, high purity, and minimal internal defects—exhibit outstanding thermal conductivity. They can be incorporated into metal-matrix composites for use as heat sinks or heat-dissipation substrates, or utilized as functional fillers in the production of thermal interface materials such as thermal pastes, adhesives, and pads.
**Preparation of Diamond Micropowder**
Currently, the primary industrial method for producing diamond micropowder is the static high-temperature, high-pressure (HTHP) synthesis followed by crushing. This process uses coarse-grained single-crystal diamond particles—synthesized via the static HTHP method—as raw material, which then undergo crushing, purification, and classification.
**(1) Preparation of Diamond Raw Material**
The HTHP method utilizes graphite powder and metal catalyst powder as primary raw materials. Under conditions of high temperature (typically 1300–1700°C) and high pressure (5–7 GPa), the catalyst facilitates a phase transition that converts the carbon source (graphite) into diamond.
**(2) Grinding and Shaping**
The grinding and shaping processes directly influence the particle morphology and the yield of the target particle size. Generally, there are two fundamental methods for reducing relatively coarse material to micron or sub-micron sizes: mechanical impact and jet milling.
(3) Classifying
Particle size classifying is a crucial step in the production process of diamond micropowder, directly influencing both production efficiency and product quality. Currently, many manufacturers employ a combination of natural sedimentation and centrifugation methods to produce a full range of micropowder grades, spanning from fine to coarse.
Thermal Conductivity Application I: The Optimal Solution for Thermal Fillers
Thermal fillers are dispersed within a polymer matrix (such as silicone or epoxy resin) to form a composite material. This material fills the microscopic gaps between heat-generating components and heat sinks, thereby reducing contact thermal resistance and establishing a continuous heat conduction network to rapidly dissipate accumulated heat. As the core raw material for thermal interface materials—including thermal grease, pads, and potting compounds—these fillers directly determine the efficiency and stability of the thermal management system.
Thermal Conductivity Application 2: High Performance Diamond/Metal Composite Materials
Based on the excellent physical properties of diamond such as high thermal conductivity, low expansion coefficient, and low density, researchers in recent years are developing metal-based highly thermally conductive composite materials using diamond particles as reinforcements. The excellent thermophysical properties of diamond/metal composite materials give it important application potential in the field of packaging.
As the demand for thermal management continues to escalate, diamond powder is poised for significant growth. With ongoing improvements in surface modification and composite processing technologies, current limitations regarding interfacial applications will be progressively overcome, positioning diamond powder to become a critical, essential material for high-end thermal management in the semiconductor industry.
Diverse Applications of Calcite and Standard Milling Solutions
Calcite is a non-metallic mineral composed primarily of calcium carbonate (CaCO₃) and has a Mohs hardness of 3. Characterized by high whiteness and chemical stability, it serves as an indispensable functional filler in sectors such as plastics, coatings, rubber, building materials, and desulfurization after undergoing grinding and processing.
There is a common misconception that the powder grinding industry is the exclusive domain of ore processing plants. In reality, manufacturers of end-use products—such as plastics, coatings, rubber, and personal care goods—are emerging as the fastest-growing segment of demand in this sector. Establishing in-house grinding lines allows companies to control powder whiteness, fineness, and moisture content directly at the source, ensuring a perfect match for their specific formulations while eliminating intermediary markups; this represents a viable strategy for reducing costs and enhancing efficiency in today's industrial landscape.
A complete calcite powder production line encompasses five key stages: crushing, drying (as required), grinding, classification and collection, and storage and packaging. The entire line operates under a sealed, negative-pressure system and offers adjustable fineness, making it suitable for the high-volume processing of standard powders. The following breakdown outlines the standardized process flow, focusing on the Raymond mill and European-style mill systems—technologies with proven track records in the industry.
1. Pre-processing: Crushing
Objective: To crush raw ore to a feed size suitable for the mill (recommended 10–30 mm), ensuring uniform feeding and creating optimal conditions for stable grinding.
Calcite has moderate hardness (Mohs hardness of 3) and requires relatively low crushing pressure:
· For primary crushing, a jaw crusher can be used to reduce large raw ore chunks to the 30–50 mm range;
· If the raw material chunks are oversized or higher production capacity is required, a secondary fine-crushing stage using an impact crusher or hammer crusher can be added. This stabilizes feed size control and prevents material blockages that could impair grinding efficiency.
Jaw crushers, impact crushers, and hammer crushers are standard auxiliary equipment for complete production lines and can be selected based on specific capacity requirements.
2. Drying (Optional/As Needed)
Calcite stored outdoors is prone to moisture absorption. When the raw material moisture content exceeds 5%, adding a drying stage is recommended to prevent material from sticking to walls or clogging the grinding chamber and pipelines, thereby ensuring continuous production.
Configuration options: Small-to-medium production lines can use an external hot-air drying furnace; large-scale lines or those in humid regions can utilize an integrated drying system that performs dewatering simultaneously with grinding for higher efficiency. Heat sources can be adapted to various furnace types, such as natural gas, biomass, or coal-fired units.
3. Core Grinding and Classification (Key Stage)
Material that has undergone crushing (and drying) is transported into the mill for grinding via a bucket elevator and a quantitative feeder. A variable-frequency dynamic powder classification system is installed at the top of the mill; the fineness of the finished product is precisely controlled by adjusting the rotor speed. Fine powder meeting specifications is carried by the airflow to the collector, while coarse particles automatically fall back into the grinding chamber for re-grinding, ensuring consistent product fineness and uniform particle size distribution.
4. Eco-friendly Negative-Pressure Dust Collection
The entire system utilizes a negative-pressure circulation process combined with a high-efficiency pulse dust collector to filter and collect dust centrally, ensuring a dust-free workshop environment and compliance with emission standards. This component is a standard feature of the production line and is essential for ensuring regulatory compliance.
5. Automated Warehousing and Packaging
The collected finished powder is stored in sealed, moisture-proof silos, with separate zones for different levels of fineness to prevent cross-contamination. Export-oriented lines can be equipped with automatic packaging machines (supporting both bulk bags and small-package formats), while internal production facilities can utilize a sealed pneumatic conveying system to transport the powder directly to the production workshop.
Applications of Aluminum Nitride in the Semiconductor Industry
Electronic Packaging Substrates
With the rise and application of power devices—particularly third-generation semiconductors—semiconductor devices are increasingly trending toward high power, miniaturization, integration, and multifunctionality. This evolution places higher demands on the performance of packaging substrates. Common ceramic materials used for electronic packaging substrates include aluminum oxide (Al2O3), aluminum nitride (AlN), silicon nitride (Si3N4), beryllium oxide (BeO), and silicon carbide (SiC).
Compared to other ceramic materials, AlN boasts superior thermal conductivity; its theoretical thermal conductivity at room temperature can reach up to 320 W/(m·K)—eight to ten times that of alumina ceramics—while thermal conductivity in actual production can reach as high as 200 W/(m·K). Additionally, AlN ceramics feature high hardness, a coefficient of thermal expansion close to that of silicon, high volume resistivity, a low dielectric constant, and low dielectric loss. Furthermore, the material is non-toxic and resistant to high temperatures and corrosion. Its comprehensive performance surpasses that of alumina and beryllium oxide, making it an ideal material for next-generation semiconductor substrates and electronic device packaging.
Semiconductor Equipment Components
Due to their unique physical and chemical properties, aluminum nitride ceramics play an increasingly vital role in the semiconductor industry. In the field of semiconductor manufacturing, the electrostatic chuck (ESC) is a critical component; its design and material selection are pivotal to the stability and efficiency of the entire production process. Given that electrostatic chucks must operate stably in plasma environments and amidst high-temperature, corrosive gases, the materials used must possess resistance to thermal shock, plasma bombardment, and chemical corrosion.
Alumina and aluminum nitride are the mainstream materials for electrostatic chucks. Among them, aluminum nitride (AlN) ceramic is considered the preferred material due to a suite of excellent properties, including high thermal conductivity, superior chemical stability, low dielectric loss and dielectric constant, and a coefficient of thermal expansion close to that of silicon. These characteristics not only ensure the structural integrity and functional stability of the electrostatic chuck under extreme operating conditions but also enhance the overall performance and reliability of the semiconductor manufacturing process. To optimize AlN ceramics for use in Johnsen-Rahbek (J-R) type electrostatic chucks, it is necessary to produce dense ceramics with a room-temperature resistivity in the range of 10⁸ to 10¹² Ω·cm at lower sintering temperatures.
Semiconductor Substrate Materials
In recent years, aluminum nitride (AlN) has emerged as a highly promising next-generation ultra-wide bandgap semiconductor and a critical strategic material, thanks to its exceptional properties. With a room-temperature bandgap of 6.2 eV, AlN possesses outstanding electrical, thermal, and acousto-optical properties that compensate for the physical limitations of first- and second-generation semiconductor materials, such as silicon and gallium arsenide.
Aluminum Nitride (AlN) Thin-Film Materials
AlN thin films are direct-bandgap semiconductor materials that exhibit excellent mechanical, electrical, and optical properties. While GaN-based blue and green light-emitting devices have advanced rapidly in recent years, the growth of GaN faces a bottleneck due to the lack of suitable substrates. Given the excellent lattice and thermal matching between AlN and GaN, the growth of high-quality AlN thin films is of great significance; they can serve as buffer layers to enhance GaN crystal quality, thereby improving the performance of devices such as detectors.
With its multi-functional properties of "heat dissipation + insulation + wide bandgap", aluminum nitride is known as the "core" of solid-state light sources, power electronics, and microwave radio frequency devices. It is the forefront of global semiconductor technology research and the focus of strategic competition. As the demand for AI computing power explodes, heat dissipation has become a core technology as important as transistor design. Although it currently faces challenges in preparation cost and process maturity, it has great development prospects in solving the "thermal management" and "high-frequency and high-voltage" bottlenecks of future semiconductors.
Behind the MLCC Shortage: Barium Titanate Is the True Lifeline
Driven by the dual engines of AI computing power and new energy, the multi-layer ceramic capacitor (MLCC) industry is experiencing a new round of supply-demand tightness.
Often referred to as the "rice of the electronics industry," MLCCs are the most widely used and ubiquitous fundamental electronic components in the sector.
As the AI server market surges, the volume of MLCCs (Multi-Layer Ceramic Capacitors) used in these systems is doubling. Demand for MLCCs in AI servers is projected to increase approximately 3.3-fold by 2030 compared to 2025 levels.
This explosive demand has directly triggered price hikes for high-end MLCCs. Furthermore, lead times have stretched dramatically—from eight weeks to as long as twenty weeks or even six months. Some reports suggest the industry may be facing the longest period of supply shortages in history.
Underpinning this situation is a critical, often overlooked component: barium titanate.
Barium titanate (BaTiO3) features a classic perovskite crystal structure and possesses properties such as a high dielectric constant, ferroelectricity, and piezoelectricity. These characteristics make it an "all-rounder" for various electronic components, earning it the title of "pillar of the electronic ceramics industry."
MLCCs (Multi-Layer Ceramic Capacitors) represent the most critical application area for barium titanate. Within an MLCC, the ceramic dielectric layer is the core component; its performance directly determines key parameters such as capacitance, voltage withstand, and frequency characteristics. Barium titanate serves as the primary raw material for this dielectric layer, accounting for approximately 70% of the raw material costs of an MLCC.
The rapid growth of emerging sectors—such as 5G, new energy vehicles (NEVs), artificial intelligence (AI), and the Internet of Things (IoT)—has driven up demands for barium titanate. For instance, MLCCs used in NEVs require barium titanate dielectric materials that have undergone specialized doping and modification to ensure stable performance across a temperature range of -40°C to 150°C. Similarly, AI devices and IoT sensors require vast quantities of miniature MLCCs and low-power memory components; this necessitates barium titanate powders with nanoscale particle sizes and high uniformity, alongside optimized ferroelectric and piezoelectric properties. The greater the AI computing power required, the more stringent the demands placed on the barium titanate used in MLCCs.
Achieving high capacitance and ultra-thin layers in MLCCs relies on the refinement of powder grains and the thinning of dielectric sheets—processes that demand high-quality core materials, advanced production equipment, and compatible manufacturing techniques.
High-end barium titanate powder is far from a simple chemical commodity; the significant technical barriers and the difficulty of expanding production capacity constitute the central challenge facing the current industry supply chain.